Add: Wanda Plaza, Fuqiao Street, Rencheng District, Jining City, Shandong Province, China
+86-18206519878
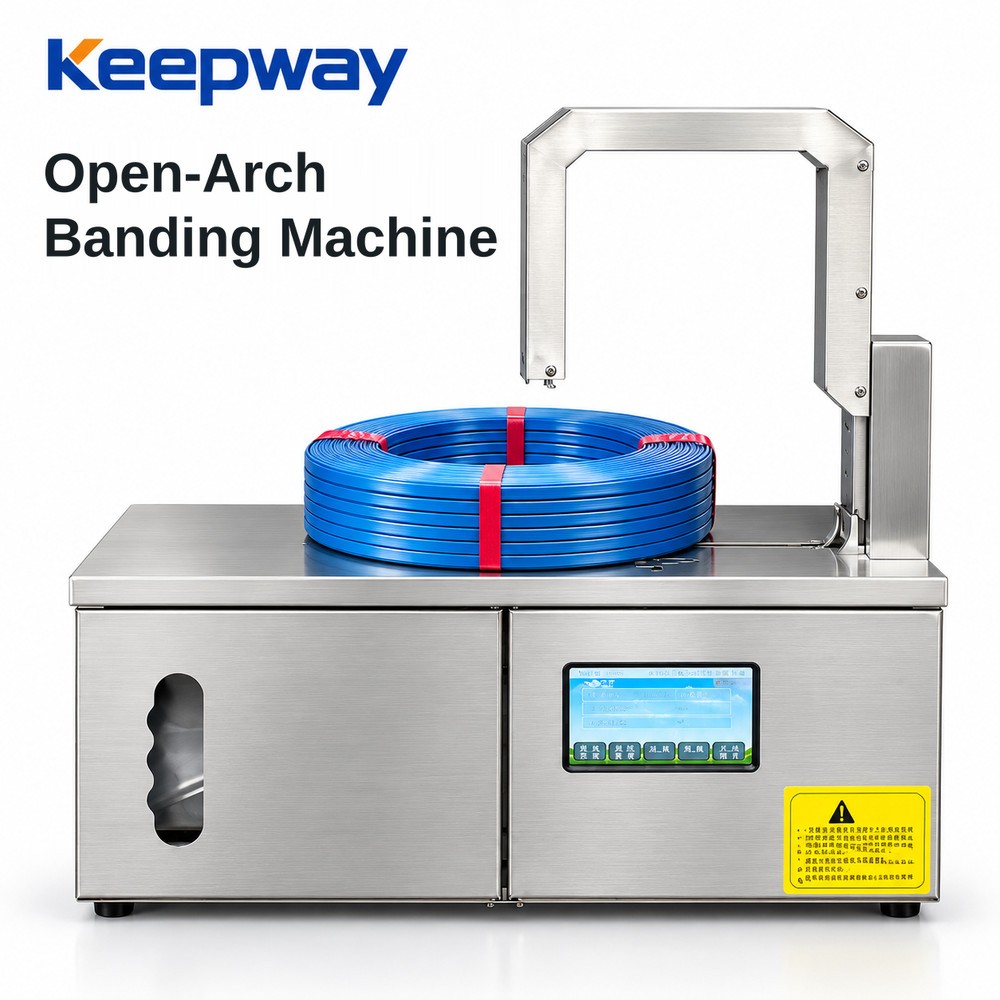
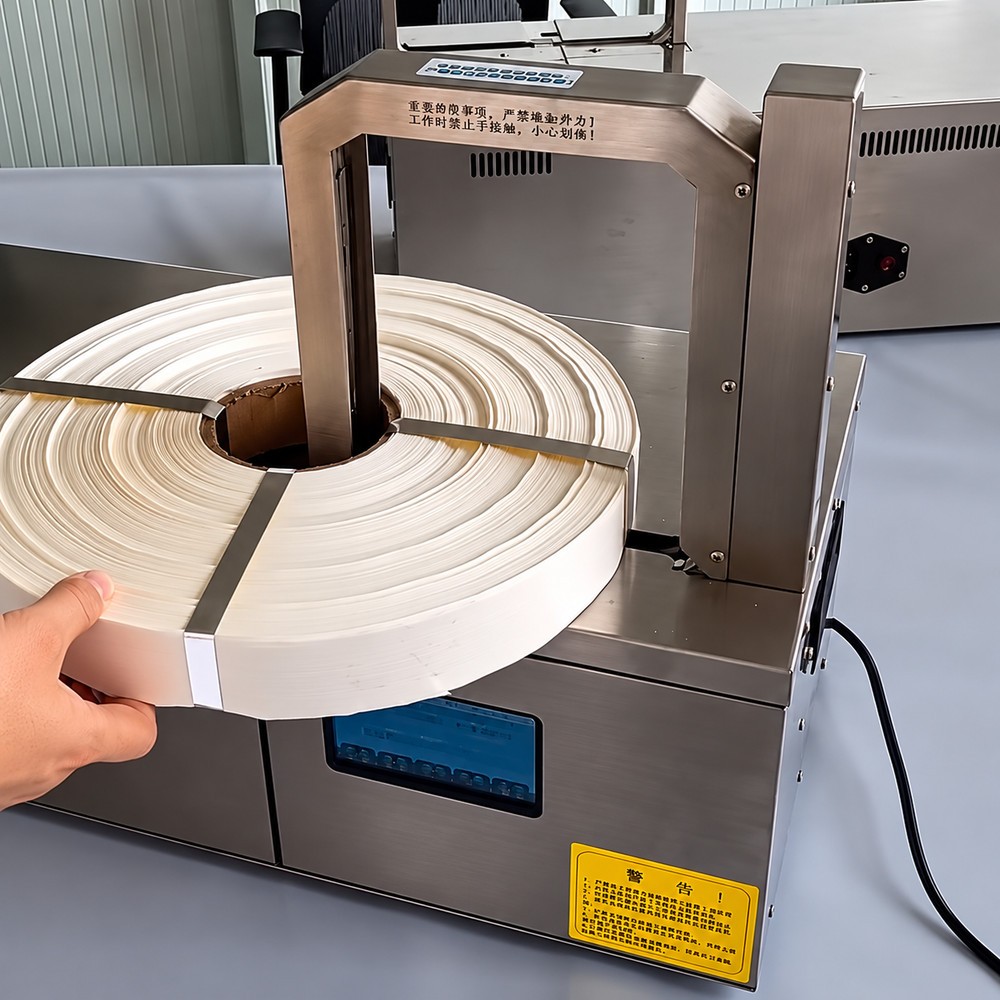
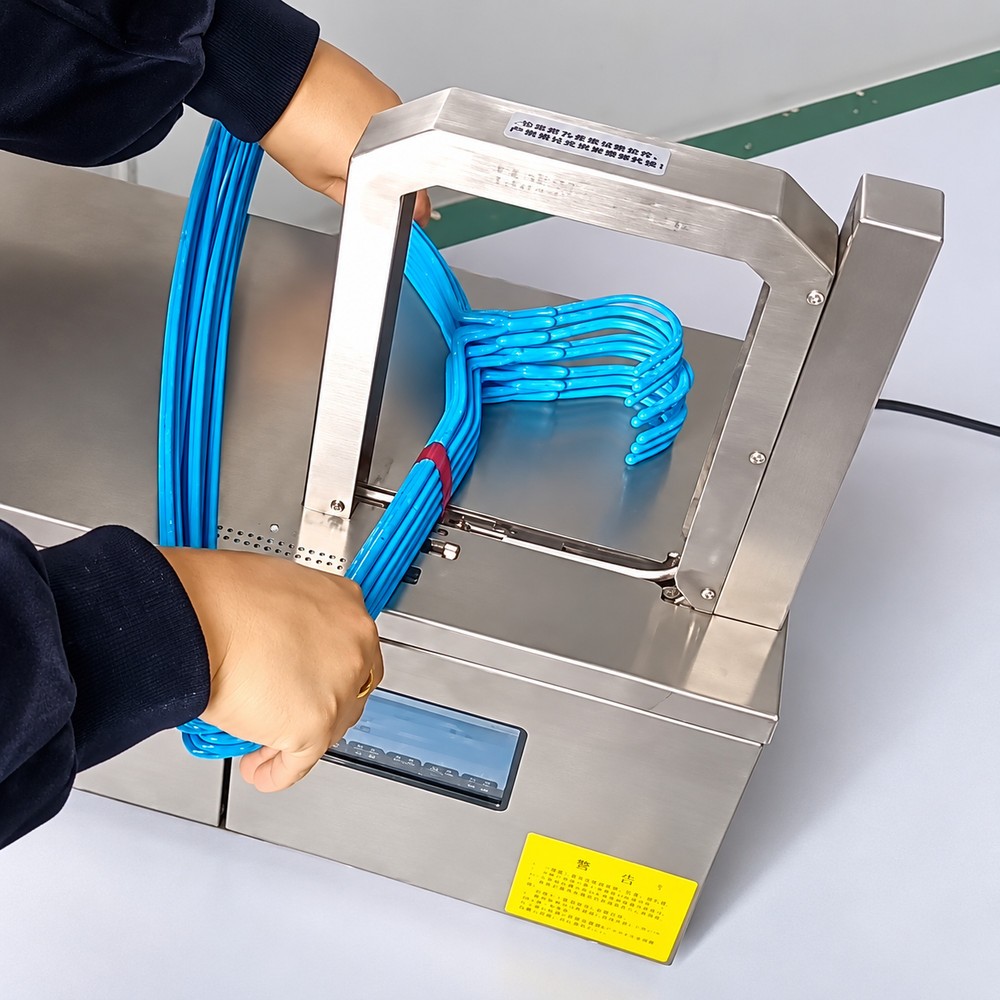
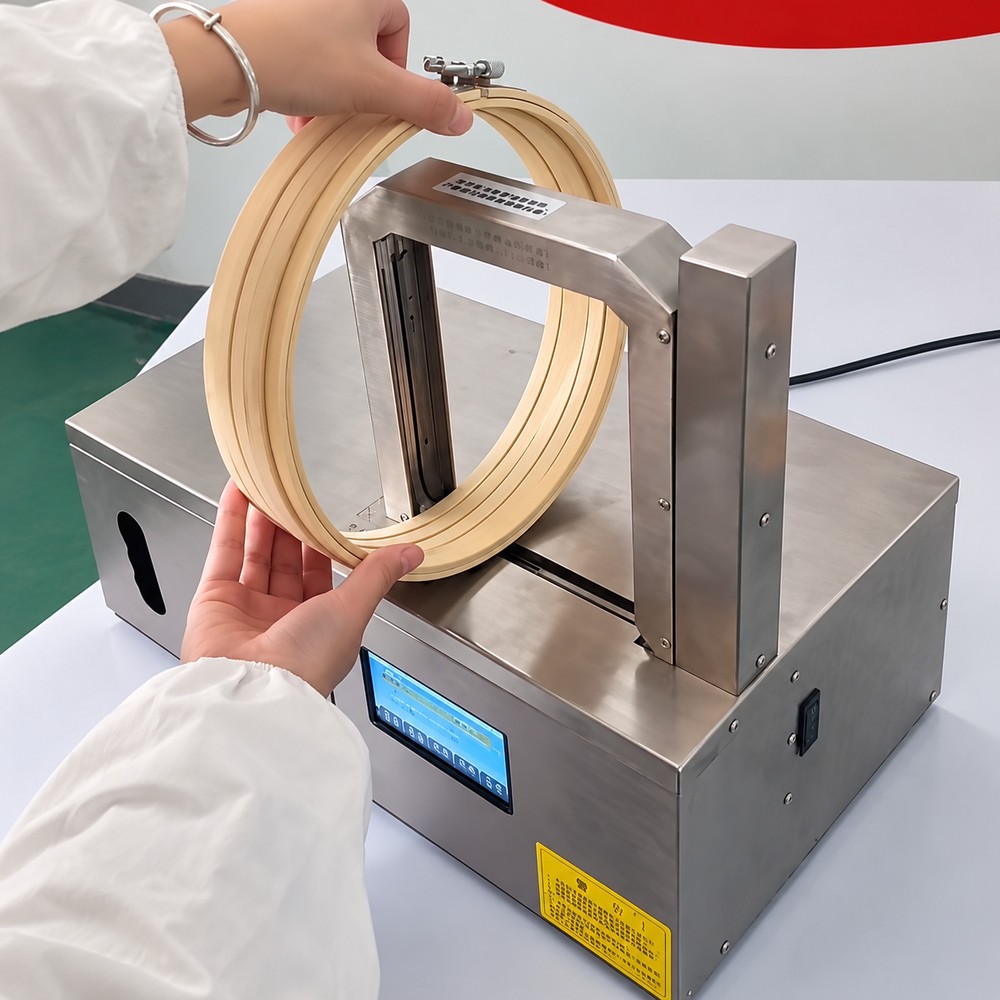
The KPW-1216 open arch banding machine is a tabletop film bander designed for a packing station where an operator needs to place a band around the local wall of a coil or another ring-shaped product. Its lift-open arch provides access for presenting a product with a centre opening. Cable coils, hose coils and tubing rings can be assessed according to their actual cross-section, flexibility and required band positions.
The important selection question is how the product sits around the arch and how the band crosses it. A large outside diameter does not describe that local banding space by itself. Send an annotated sample photo before choosing a configuration.

A coil bander must be checked against both access and the section enclosed by the band. The centre opening affects whether the product can be presented around the arch for through-the-eye coil banding, with separate bands placed at the required locations. The radial wall and stack height affect the banding cross-section. The outside diameter affects handling space around the machine. These dimensions should be shown separately in a quotation request.
| Information to send | Why it matters |
|---|---|
| Outside diameter and centre-opening diameter | Checks product access, orientation and handling space. |
| Local coil-wall width and axial stack height at the band location | Defines the section that the band must enclose. |
| Product weight, stiffness and tendency to spring open | Helps assess presentation, support and band retention during handling. |
| Number, position and orientation of bands | Defines the complete packing task, including manual repositioning. |
| Surface finish and acceptable compression | Helps select a film band and trial settings without assuming all surfaces behave alike. |
The 120 mm limit applies to the local coil wall or wire-bundle section being banded. It is not a 120 mm limit on the outside diameter of the complete coil. The supplied specifications show a 120 × 180 mm window; KEEPWAY must also check the actual insertion clearance and product orientation with the sample.
The openable arch provides access for presenting a product around the banding area. It is useful when a ring-shaped item cannot be treated as a solid carton passing straight through a fixed arch. Confirm the loading orientation with the actual sample; a photograph of a coil alone cannot establish working clearance.
Final access and clearance at the openable arch and band guide are assessed with the proposed product orientation.
The banding mechanism feeds film around the local section, tensions the band, and forms a heat-sealed joint before cutting. The film structure, tension and sealing settings must be matched to the sample. A finished band should be checked for joint consistency, retention and the effect on the product surface.
The feed, sealing and cutting mechanism must be assessed with the actual band and product; no joint-strength rating or complete packing throughput is established by an illustration.
The supplied control-panel reference includes adjustment fields for band tension, sealing time and band length. These are setup variables for an approved product-and-band combination. Screen example values are not a universal operating recipe.
Use the approved touchscreen settings for the actual film and product rather than copying a value from an illustration.
For cable and hose coils, assess the coil-wall section and whether the band holds the intended bundle during the required handling step. For tubing rings, include spring-back and surface requirements. Hanger stacks and wooden hoops illustrate other presentation shapes, but each needs its own sample assessment.
Assess each application with a sample check for size, weight, stiffness and the intended handling task.

The values below come from the supplied product material and the confirmed model, local-section definition and supply policy. They are reference specifications, not independent test results. Confirm the ordered configuration and sample fit in the quotation; the reference opening dimensions do not replace a clearance check with the actual product.
| Item | KPW-1216 reference | How to apply it |
|---|---|---|
| Model | KPW-1216 | Open arch film bander for the local section of a coil or ring-shaped product. |
| Local section limit | 120 mm | Applies to the sidewall or wire-bundle section being banded, not the complete coil outside diameter. |
| Reference working window | 120 × 180 mm | Check actual product insertion, centre opening, orientation and clearance with a sample. |
| Band tension | 10–90 N reference range | Approve a suitable setting for the film, retention requirement and product surface. |
| Film band | 12 mm wide; 0.10–0.15 mm thick | Confirm the laminate and the approved band sample rather than assuming every film of the same width is compatible. |
| Film structures shown | CPP + PET + CPP or OPP + PET + OPP | These are film laminates; they do not establish compatibility with thick PP/PET transport strap or paper bands. |
| Joint formation | Heat sealing | Approve the joint and band retention on the intended sample. |
| Machine cycle reference | 1.5 seconds per cycle | Excludes manual loading, positioning, rotation/repositioning and unloading. It is not finished coils per minute. |
| Nominal overall size, arch closed | 460 × 260 × 420 mm (L × D × H) | Reference machine envelope; allow additional product and operator handling space. |
| Nominal overall size, arch raised | 460 × 260 × 580 mm (L × D × H) | Raised reference envelope, not a stated maximum bundle height or lift-stroke specification. |
| Electrical supply | AC 220 V reference | Voltage and frequency are configured to customer requirements and confirmed in the quotation/order. |
| Heating reference | 350 W instantaneous heating | This is the heating figure, not a stated whole-machine rated input power. |
The KPW-1216 is presented as a heat-sealing film bander. Select the band structure and dimensions against the machine configuration and the sample test. Do not substitute an ordinary tape simply because its nominal width looks similar. Include an existing film sample or its material specification when replacing a current banding process.
The quotation should state KPW-1216, the approved working space, film-band specification, ordered voltage and frequency, and included configuration. If a support arrangement or integration into another process is required, describe it as part of the project so its scope can be checked separately.
Machine-cycle time and complete packing time describe different things. A multi-band coil may require several presentations and manual repositioning. Request a sample demonstration of the complete task when comparing output requirements.
Outside diameter is one part of the check. Supply the centre opening, local coil-wall width, stack height, weight and a photo showing the intended band path. The product must fit around the arch in the proposed orientation, with sufficient insertion and handling clearance.
This page describes a tabletop banding station with operator presentation. If your process needs automatic infeed, rotation or transfer, provide the required sequence so a separate integration scope can be assessed.
Choose the process from the required pack. A local heat-sealed film band has a different task from heavy carton strapping, transport-load restraint or full-surface stretch wrapping. Send the intended handling and protection requirements before selecting equipment.
That depends on the sample, the number of bands and the presentation and handling sequence. A trial of the whole job provides a more useful basis than converting a single machine-cycle figure into finished coils per minute.
These short demonstrations show operator presentation of the coil. Clip duration is not a machine-cycle or completed-coil production-rate specification.
Send product photos, outside and inside dimensions, local banding cross-section, weight, band positions, surface requirements, target completed output, site supply and destination. If you already use film bands, include their material and dimensions. KEEPWAY can then assess the packing task and prepare a configuration for the actual sample.
Mobile:+86-18206519878
Tel:+86-18206519878
Whatsapp:8618206519878
Email:sales@kbwmachinery.com
Add:Wanda Plaza, Fuqiao Street, Rencheng District, Jining City, Shandong Province, China